bushings and sleeves
Custom Bushings & Sleeves — Steel, Brass & Stainless
We manufacture bushings and sleeves to your drawing — turned, milled and finished in one factory, with a material certificate and pre-shipment photos before the goods ship.
Upload your drawing (STEP, IGES, DWG, DXF, PDF) — we return DFM feedback and a quote within 24 hours.
- Tolerance
- ±0.01 mm
- MOQ
- From 50 pcs
- Sample
- 5–10 days
- Production
- 25–35 days
- Documents
- MTR + pre-shipment photos
What this part is and where it is used
Bushings and sleeves are hollow cylindrical parts with a precise inside and outside diameter, used to guide, support, space or reduce wear between a shaft and a housing. They are machined to your drawing, with the bore and the outside diameter held to ±0.01 mm on precision features, so the ID, OD, length, wall thickness and material are set by the print. Unlike a threaded fastener, a bushing usually has no thread — it presses or slides into position and lets a shaft turn or move through it.
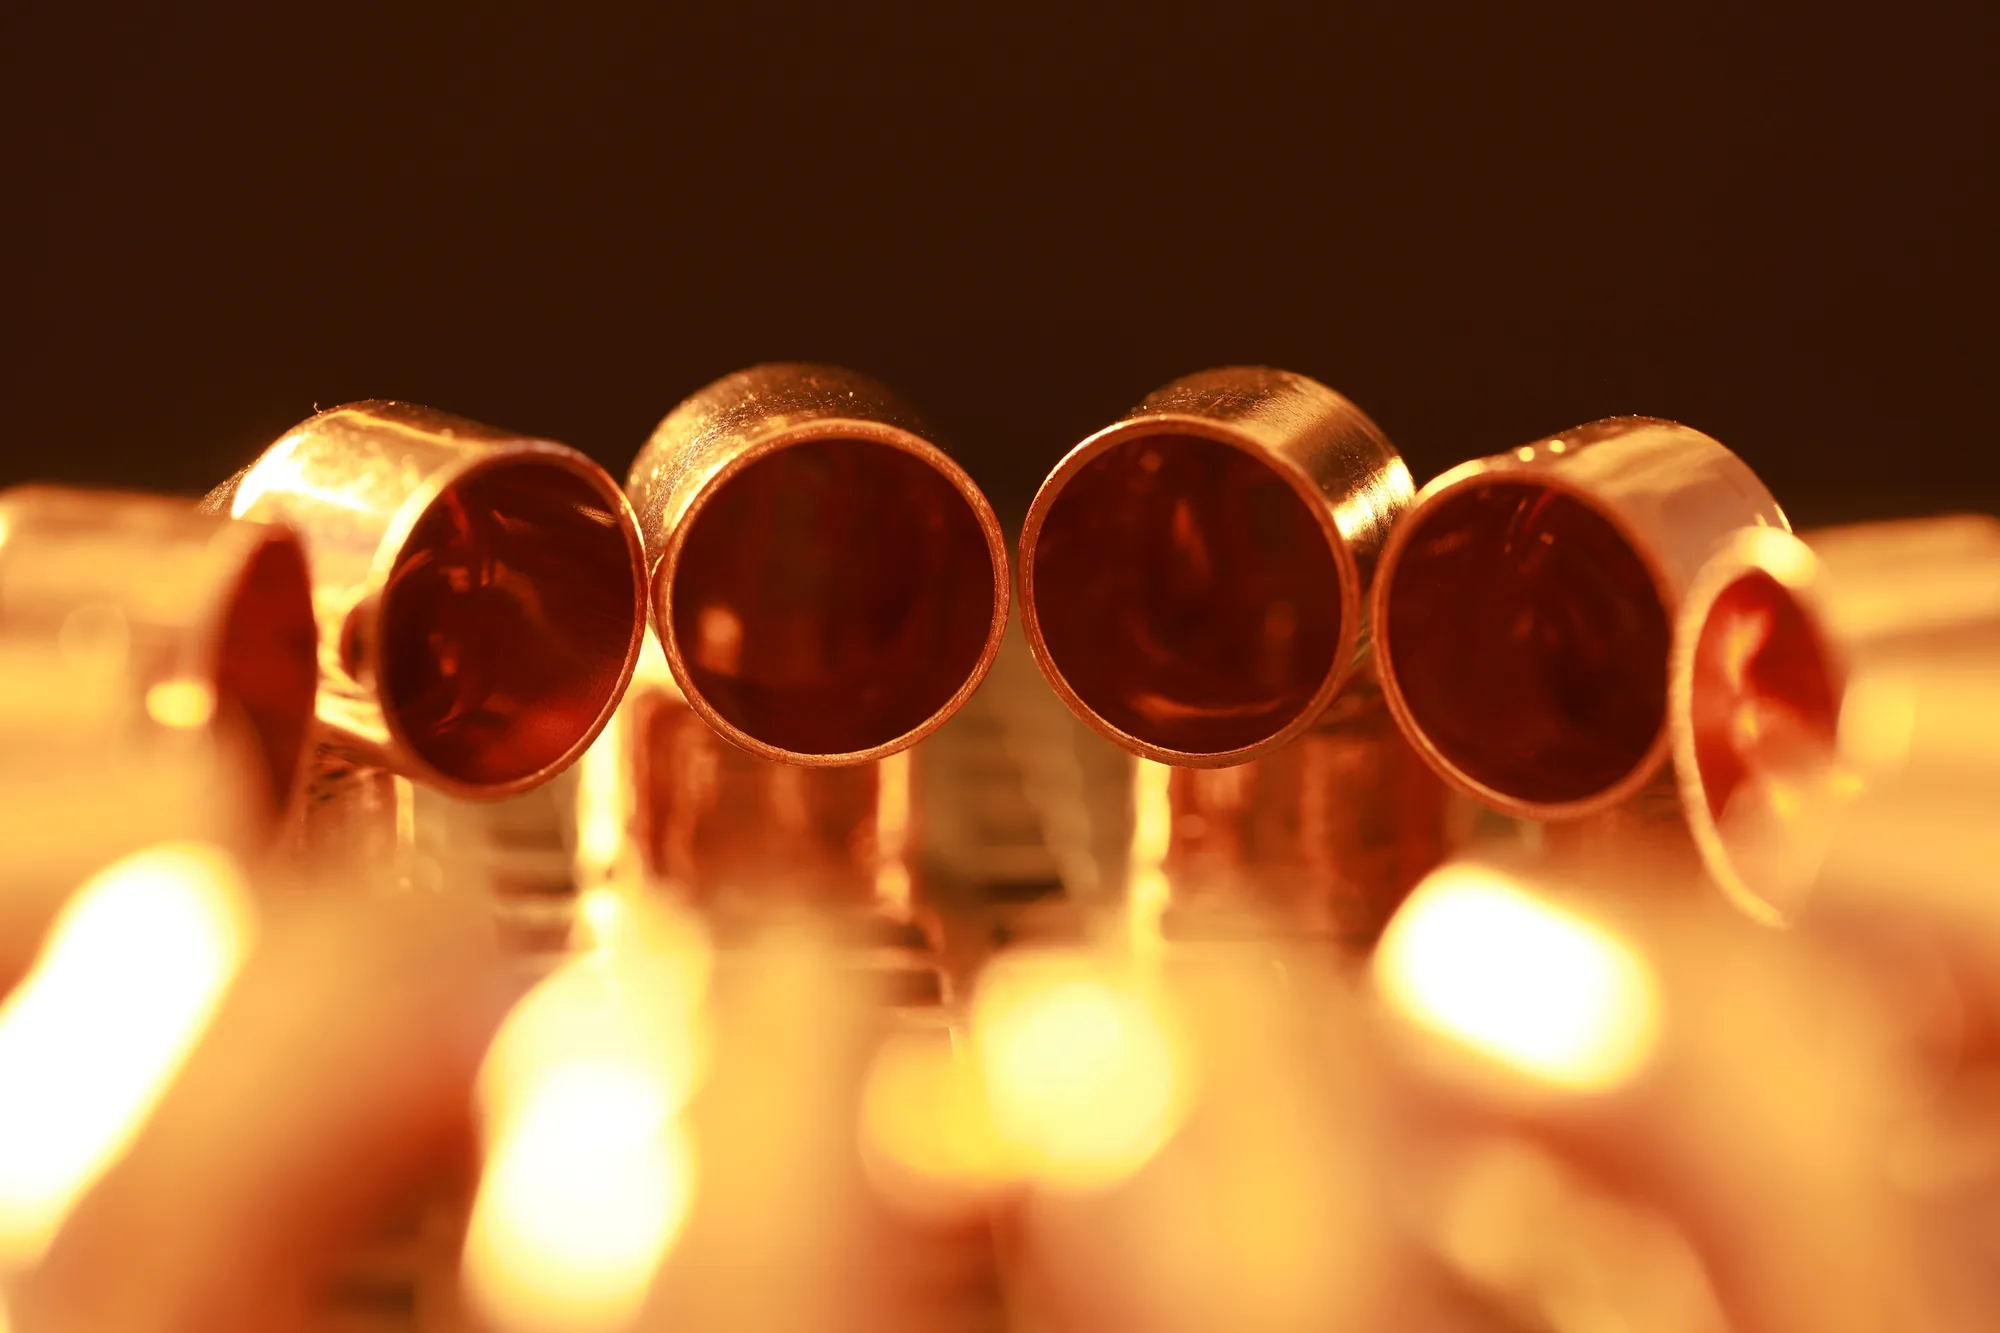
Buyers order custom bushings and sleeves when a catalog size or material does not fit: a non-standard bore, a flange for axial retention, a split for easier fit, or a bearing alloy such as brass or copper. They are common in pivots, linkages, shafts and mounting blocks.
Types of bushings and sleeves we manufacture
We machine the common forms to print:
- Plain bushings — straight cylindrical sleeves.
- Flanged bushings — a collar on one end for axial location.
- Split sleeves — a slit along the length for easier fit and retention.
- Shouldered and stepped sleeves with custom walls and steps.
Some buyers raise sleeve bolts and sleeve anchors — including stainless sleeve anchors and stainless steel sleeve anchors — in the same conversation. Those are threaded fasteners for structural mounts, while this page covers the plain cylindrical bushing and sleeve itself. For the threaded side, see our custom fasteners pages.
Bushing types
We cut the styles that fit how the part mounts and wears:
- Plain sleeves — straight cylindrical bushings with a single bore and OD.
- Flanged bushings — a collar on one end locates the part axially against the housing face.
- Split sleeves — a slit along the length eases fit and helps the sleeve grip once pressed in.
- Shouldered bushings — a step or multiple diameters for locating and seating in a bore.
- Bronze bushings — a copper-alloy bearing surface, machined from our brass and copper family for wear-facing pivots.
Every form starts from bar on our floor, so the bore, OD, wall and flange all follow your drawing. They are a natural pairing with custom shafts and locate parts in machine fixtures.
Bore, OD and concentricity
The bore, outside diameter and length are set by your drawing, and because we cut the bore and OD in one setup the two stay concentric to the print. Precision features such as the bore or a locating diameter are held to ±0.01 mm, and general dimensions to ISO 2768-m unless your drawing states otherwise.
A bushing lives or dies by how the bore runs to the OD, so we machine both from the same holding rather than trusting a second setup. Tell us which surface the shaft rides on and we hold that surface to the tighter end of the drawing — see our tolerances and drawing requirements pages.
Materials, threads and finishes
Common materials are brass, bronze and copper for bearing and wear surfaces; aluminium 2024, 5052, 6061 and 7075 for light weight; stainless steel 303, 304, 316, 316L and 17-4PH for corrosion and strength; carbon and alloy steel 1045, 1215, 4140, D2 and O1 where the sleeve takes load or wear; and titanium for weight-critical parts. See our materials index, brass and copper parts, stainless steel parts, aluminium parts, steel parts and titanium parts pages.
Most bushings are unthreaded, but a threaded sleeve follows metric or inch references — see our thread standards guide. Finishing runs through our vetted partner network under one quality process: passivation for stainless steel, anodizing for aluminium and black oxide for steel, among others. Wall thickness and concentricity are held to the print, so the bushing presses or slides into its housing the way the drawing intends.
Bushing or bearing: which one belongs in the joint
A plain bushing and a rolling bearing both support a rotating or sliding shaft, and they are chosen for opposite reasons.
A plain bushing is a single part with no moving elements. It handles high load at low speed, takes shock and vibration without brinelling, runs in dirty or submerged conditions where a rolling bearing would contaminate, and costs little to replace. Its weakness is friction: it runs hot at speed, and it needs lubrication to survive.
A rolling bearing carries less load for its size but far less friction, so it suits continuous rotation at speed. It is also less tolerant of shock, misalignment and contamination.
The practical crossover is usually speed against load. A pivot that rocks a few degrees, a linkage that moves slowly, a pump shaft in washdown duty, a conveyor roller that turns at a few hundred rpm — those are bushing applications. A spindle turning at thousands of rpm is a bearing application.
There is a second reason a bushing wins even where a bearing would fit: envelope. A thin-wall bushing can be fitted into a housing where there is no room for a bearing’s outer ring and its shoulder, and it can be sized to a bore that a standard bearing does not come in.
Press fit: what the housing has to be
A bushing usually holds its position by interference in the housing, and the amount of interference is a designed number rather than a workshop preference.
For a light press on a 20 mm outside diameter, an interference of about 0.02 mm to 0.05 mm is the working range. Below that the bushing can walk or rotate in service; above it the housing may split, particularly in a casting, and the bore of the bushing closes in as the material is compressed.
The convention is to specify the housing bore and the bushing outside diameter as fit pairs rather than as single figures — an H7 housing with a p6 or s6 bushing outside diameter, for example. A drawing that gives the bushing OD as a nominal with no tolerance hands the decision to the shop, and the shop will pick something safe rather than something correct.
Interference closes the bushing bore, so the bore has to be machined with that closure in mind. On a thin-wall bushing in a press fit, the bore can come in by a few hundredths of a millimetre once the part is installed. Where the running clearance matters, the drawing should say whether the bore is dimensioned before or after fitting, because the two are not the same size.
Running clearance, fits and lubrication
Once the bushing is in place, the shaft has to run in it with the right clearance, and clearance is set by the application rather than by a general rule.
A shaft running slowly with occasional movement can take a clearance of 0.05 mm to 0.10 mm on a 20 mm diameter. A shaft rotating continuously wants less — commonly 0.02 mm to 0.05 mm on the same size — because excess clearance lets the shaft orbit, which raises noise and wear. A shaft that has to locate accurately wants less still, and then lubrication becomes critical because there is less room for an oil film.
Lubrication grooves are how a bushing keeps oil where the load is. A spiral groove distributes oil along the bore; straight axial grooves feed it in from the ends; a figure-of-eight pattern holds it in the loaded zone. Whatever the pattern, the groove should stop short of the bushing ends — a groove that runs out to the edge lets the oil escape instead of holding it.
Porous bronze, commonly called oil-impregnated bronze, is a different product from a machined bronze bushing. It is sintered from powder, and the porosity that holds the oil is the reason it works. Machining the bore of a sintered bushing closes the surface pores and removes most of the benefit, so it is bought to size rather than cut to size.
Flange, shoulder and step: how the part is retained
A plain cylindrical bushing can move axially unless something stops it, and there are four common ways to stop it.
A flange is a collar on one end that bears against the housing face. It locates the bushing axially, gives a surface for the assembly to seat against, and can also act as a thrust washer if the flange face is sized for it. The flange thickness is a load-bearing dimension, not a cosmetic one — a thin flange on a joint with axial load will deform.
A shoulder, or step, is a change in outside diameter partway along the bushing. It seats the part in a counterbore, so the bushing is located by the housing geometry rather than by a collar.
A retaining compound or a light interference at one end holds the bushing where the housing cannot be machined with a shoulder. It is the least positive method and the one most dependent on surface condition.
A split in the wall lets the bushing compress on fitting and grip once in place, which retains it without any shoulder at all — useful where the housing has to be bored straight through.
Where the bushing also has to take thrust, say so on the drawing. A bushing sized only for radial load and then used as an axial stop will wear on its end face, and the end face is usually the least controlled surface on the part.
Split sleeves and where they earn their cost
A split sleeve has a slit cut along its length, and it is specified for one of three reasons.
The first is assembly. A split sleeve compresses slightly as it is pressed in, so it can be fitted into a bore that would otherwise need a heavier press or a heated housing. On a serviceable assembly, that matters.
The second is take-up. As a bushing wears and the clearance opens, a split sleeve retains some ability to close and hold the shaft, which extends the interval between replacements.
The third is clamping. A split sleeve with an external clamp or a taper converts a radial squeeze into a grip on the shaft, which is how split collets and clamping sleeves work.
The cost is concentricity. A split sleeve is no longer a closed ring, so its bore-to-OD relationship changes as it is compressed, and it will not hold the runout that a solid bushing holds. Where the shaft has to locate precisely, a solid bushing is the correct choice even if it is harder to fit.
Wear: which material pairing survives
A bushing is a sacrificial part, and which one wears is decided by the material pairing rather than by the material of the bushing alone.
Two identical materials running against each other are the worst case. Steel on steel without adequate lubrication will gall — microscopic welds form and tear — and the surfaces fail quickly. The usual answer is to make one part softer and, where possible, to use a material with natural lubricity. Bronze, brass and copper alloys running against steel are the classic pairing for exactly this reason.
A hardness difference helps but does not replace lubrication. A bearing bronze against a hardened shaft wears predictably and can be replaced when the clearance opens; the shaft, being harder, survives. Reversing that — soft shaft, hard bushing — moves the wear to the more expensive part.
Load and speed together set the limit. A bronze bushing in a slowly oscillating pivot carries a much higher pressure than the same bushing running continuously, and the permissible pressure falls as surface speed rises. Where a joint runs fast and loaded, the answer is usually more bearing area rather than a harder material.
Where the environment is corrosive or the joint is submerged, stainless against stainless is the pairing to avoid — it galls readily and has no hardness differential. A bronze or polymer bushing against a stainless shaft is the usual solution.
What the drawing has to define for a bushing
A bushing drawing that comes back right the first time answers six questions.
The bore and the outside diameter, each with its tolerance, and a statement of which one governs. On most bushings the bore is the functional surface and the outside diameter exists to hold it, but on a press fit the outside diameter sets the interference that decides the finished bore.
The length, and whether it is a free dimension or a locating one. A bushing that sets the gap between two components has a length tolerance; one that is simply a bearing surface usually does not.
The concentricity between bore and outside diameter, expressed as total indicated runout against a datum rather than as a note.
The material, by grade. “Bronze” leaves the choice between a bearing bronze and a decorative one, and they behave differently under load.
Any groove, flat, slit or hole, with its position and size. A lubrication groove that is not dimensioned will not be where the designer expected it.
The fit it is going into. Naming the housing bore tolerance on the bushing drawing lets the shop hold the interference the design needs, rather than assuming a general press.
Bushing drawing mistakes we see
Five errors come back on bushings often enough to name.
A bore and outside diameter with no concentricity call-out is first. The part is then made to two independent diameters, and the runout is whatever the setup produced.
Second is a press fit specified without saying whether the bore is measured before or after fitting. On a thin wall the two differ by more than the bore tolerance.
Third is a groove that runs out to the end of the bushing. It looks correct on the drawing and it holds no oil.
Fourth is a wall too thin to machine. Below about 1 mm on a small diameter, the part deflects under clamping and cutting pressure, and the bore comes out lobed rather than round. Where the wall has to be thin, the drawing should expect a support or a finishing pass.
Fifth is a material chosen by colour rather than by function — a “bronze” bushing ordered for a wear application may come back as a decorative alloy with no bearing properties at all.
How bushings and sleeves are priced
Bushing pricing follows three lines, and on small parts the material and the bore dominate.
Material is a function of the bar diameter, which has to exceed the outside diameter, and of how much of the bar ends up in the part. A bushing is nearly all hole, so utilisation on a large-OD, small-bore part is poor and the material line is high relative to the finished weight.
Machining time is driven by the bore. A through bore is fast; a blind or stepped bore, an internal groove, or a bore held to a tight tolerance with a concentricity call-out adds operations. Where the bore is the functional surface and the outside diameter is merely a holder, the routing can sometimes be reversed — outside diameter first, then bore from the same setup — and the drawing should allow it.
Quantity sets how the setup is spread. Orders start from 50 pieces, samples take 5–10 days and production 25–35 days, with monthly capacity over 100,000 parts. Send the drawing with the fit and the material and we return a quote within 24 hours with DFM feedback, including where a different wall, a different alloy or a solid instead of a split form would serve the joint better.
Industries and applications
Bushings and sleeves appear in automotive, aerospace, oil and gas, hydraulic and pneumatic and agriculture assemblies. They guide shafts in pivots, linkages and pumps, while flanged bushings locate parts axially in mounting blocks and machine fixtures.
Types and variants we manufacture
We manufacture the full spacer and standoff family from bar stock, with every part cut to drawing.
- Round and hex standoffs — the two most common bodies; hex gives wrench access for tightening.
- Male-female standoffs — a threaded stud on one end and a tapped hole on the other, for chaining or panel mounting.
- Female-female standoffs — tapped at both ends, for joining two screws through panels.
- Male-male and through-bore standoffs — studs or plain bores for specific mounting arrangements.
- Shoulder spacers — a locating step that positions the part radially while setting the distance.
- Tube spacers — thin-wall spacers for light, low-cost separation.
- Swage (press-in) standoffs — pressed permanently into a panel for board-to-board mounting.
Each part is defined by your print: outside diameter, length, thread, wrench flat size and any shoulder or counterbore. Where a drawing needs more than a straight bore, we add counterbores, cross-holes, chamfers and wrench flats in the same turning cycle. See our fastener specifications guide for the dimensions to include.
Why order this part from our factory
Your spacers and standoffs are produced end to end in our own factory in Qidong City, Jiangsu Province, China — turned, milled and finished without handing the job between facilities. We quote within 24 hours with DFM feedback, so a question on a thread depth or a wrench flat is resolved before you order. The minimum order is from 50 pieces and samples start from 1 piece; sample lots ship in 5–10 days and production in 25–35 days after sample approval, with over 100,000 parts of monthly capacity available. Every shipment leaves with a material certificate (MTR) and pre-shipment photos. Send your drawing or a sample through request a quote and we will return a price and lead time.
Specifications
| Bushing types | Plain sleeve · flanged · split · shouldered · bronze — per drawing |
|---|---|
| Bore & OD | Bore, outside diameter and length per drawing |
| Materials | Brass & bronze & copper · aluminium 2024 / 5052 / 6061 / 7075 · stainless steel 301 / 303 / 304 / 304L / 316 / 316L / 410 / 416 / 17-4PH · steel 1045 / 1215 / 4140 / D2 / O1 · titanium |
| Tolerance | ±0.01 mm precision features · ISO 2768-m general unless stated |
| ID range | 2–100 mm, honed to H7 |
| Wall thickness | 0.5–15 mm |
| Secondary | Oil grooves, press-fit chamfer, reaming |
| Lot size | 50–20,000 pcs |
| General tolerance | ISO 2768-m unless stated on the drawing |
| Forms | Round, hex and square spacers and standoffs |
| Configurations | Male-female, female-female, male-male and through-bore |
| Threads | Metric and inch (UNC/UNF), internal and external per drawing |
| Length | Cut to drawing length; no catalogue increments |
| Finishes | Anodising, zinc and nickel plating, black oxide, passivation |
| Mounting | Board-to-board, panel-mount and press-in (swage) styles |
| Samples | 5–10 days |
| Quote | Within 24 hours with DFM feedback |
| Capacity | Over 100,000 parts per month |
Frequently asked questions
What is the minimum order quantity for bushings and sleeves?
We start from 50 pieces per style and material, so a first run or prototype batch stays practical before you order production quantities.
What are your lead times?
Sample bushings and sleeves take 5–10 days and production runs take 25–35 days after drawing approval. We return DFM feedback with your quote within 24 hours.
What tolerances can you hold on a bushing or sleeve?
General work is machined to ISO 2768-m unless your drawing states otherwise, and precision features such as a bore or locating diameter are held to ±0.01 mm.
Which materials do you machine bushings from?
Brass, bronze and copper for bearing surfaces; aluminium 2024, 5052, 6061 and 7075; stainless steel 303, 304, 316, 316L and 17-4PH; carbon and alloy steel 1045, 1215, 4140, D2 and O1; and titanium.
Can you make flanged or split sleeves?
Yes. We machine plain, flanged, split, shouldered and stepped sleeves to print, including custom walls, steps and axial locating collars.
Do you make threaded sleeves?
Yes — a sleeve with an internal thread follows [metric](/metric-fasteners/) or [inch](/inch-fasteners/) references as your drawing states. Most bushings are unthreaded, but a threaded sleeve is within our range.
What is the difference between a bushing and a sleeve anchor?
A bushing or sleeve is a plain cylindrical part that guides or spaces a shaft, while a sleeve anchor is a threaded fastener for structural mounts. For the threaded side, see our [custom fasteners](/custom-fasteners/) pages.
Do you provide material certificates?
Every batch ships with a material certificate (MTR) for the raw material and pre-shipment photos of the finished parts before dispatch.
Can you machine a flanged or split bushing to my drawing?
Yes. Plain, flanged, split, shouldered and bronze bushing styles are cut to your print — bore, OD, wall and flange dimensions all follow the drawing. Upload a STEP, DWG or PDF and we return DFM feedback with a price within 24 hours.
How concentric can you hold the bore to the outside diameter?
The bore and OD are cut in one setup on our floor, so concentricity follows from a single holding. Precision features are held to ±0.01 mm and general dimensions to ISO 2768-m unless your drawing states otherwise.
Which materials suit a bushing or sleeve?
Brass, bronze and copper for bearing and wear surfaces; aluminium 2024, 5052, 6061 and 7075; stainless steel 303, 304, 316, 316L and 17-4PH; carbon and alloy steel 1045, 1215, 4140, D2 and O1; and titanium — see our [brass and copper parts](/brass-copper-parts/) and [stainless steel parts](/stainless-steel-parts/) pages.
Are you a factory or a trading company?
We are our own factory in Qidong City, Jiangsu Province, China. Bushings and sleeves are turned, bored and milled on our own floor — from bar, tube or plate depending on the wall thickness and the material — and never resold from stock. See our [factory](/our-factory/) page.
How do I get a quote for bushings and sleeves?
Upload your drawing (STEP, IGES, DWG, DXF or PDF) through the [quote form](/request-a-quote/) or send it on WhatsApp. We reply with DFM feedback and a price within 24 hours.
What is the difference between a spacer and a standoff?
A spacer is a plain unthreaded part that sets a distance, while a standoff is threaded so panels or boards can be screwed onto it.
Can you make hex and round standoffs?
Yes, round, hex and square standoffs are all produced to your drawing in the thread and length you specify.
Do you offer male-female and female-female configurations?
Yes, male-female, female-female, male-male and through-bore styles are all available, plus press-in swage standoffs for panels.
Can you make shoulder and tube spacers?
Yes, shoulder spacers with a locating step and thin-wall tube spacers are both turned to drawing.
What materials are available?
Aluminium 2024, 5052, 6061 and 7075; stainless steel 301, 303, 304, 316 and 316L; carbon steel 1045 and 1215; alloy steel 4140; brass, copper and bronze; and engineering plastics where the spacer has to insulate.
Send your drawing — quote in 24 hours
DFM feedback, material certificates and pre-shipment photos come with every order.